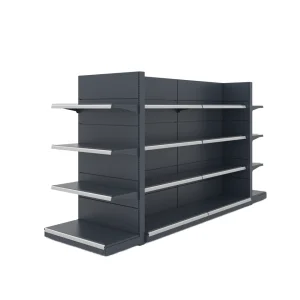
Direct from factory production lines, engineered to industrial CE standards for durability, utility, and modern store aesthetics.
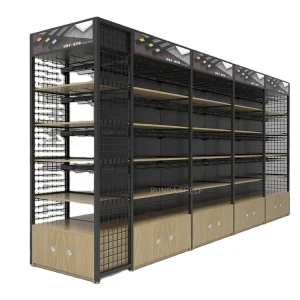
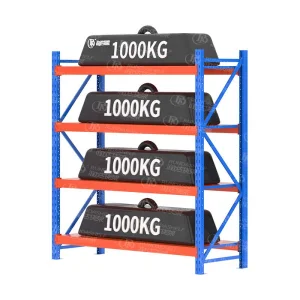
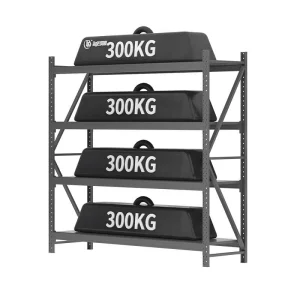
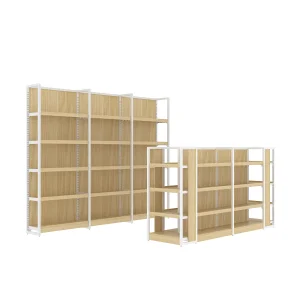
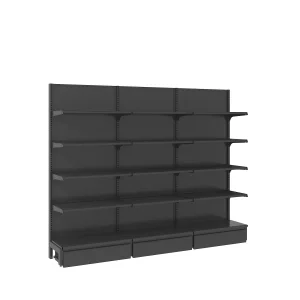
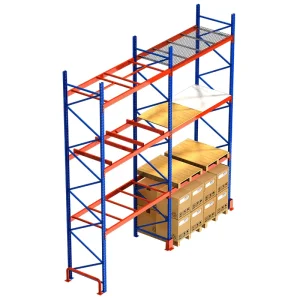
The global retail landscape is undergoing a massive transformation, moving from static cashier-centric layouts to fluid, automated transaction zones. Modern checkout counters are no longer just point-of-sale platforms; they are central to optimizing retail floor efficiency, mitigating shrinkage, and driving high-value customer interactions. Strategic alignment with ergonomic engineering and hardware integration is critical for modern commercial environments.
Seamless engineering of POS brackets, weight sensor beds, cash modules, and payment terminals to facilitate rapid transactions.
Mitigating cashier strain through height-adjustable belts, custom control console panels, and intuitive cash wrap pathways.
Transitioning to long-lifecycle recyclable steel alloys, high-impact polymers, and eco-friendly powder-coating formulations.
For global procurement entities and regional developers, sourcing modular cashier units with high scalability is vital. Systems must adapt to peak seasonal traffic, shift configurations dynamically, and support legacy and futuristic retail scanning hardware without structural redesigns.
Enterprise procurement professionals look beyond the ticket price when securing logistics and retail equipment. The primary metric is Total Cost of Ownership (TCO), driven by long-term durability, structural integrity, and local regulatory compliance. Purchasing managers from the Middle East, South America, and Eastern Europe prioritize structural safety standards like CE and ISO certification to ensure resilience against high-traffic impacts, structural fatigue, and corrosion.
A highly integrated manufacturer and global trading hub providing structural reliability, intelligent design, and elite industrial engineering.
Founded in 2016, Chengdu CoreStorage Logistics Equipment Manufacturing Co., Ltd. spans a comprehensive factory area of 22,000 m², generating an annual export revenue of $15,000,000. We bring 6 years of global trade expertise alongside 11 years of specialized industrial rack manufacturing experience.
To ensure maximum load integrity, our quality control procedures adhere to ISO 9001 & CE Structural Safety Standards, utilizing advanced CMM Automated Dimensional & Load Stress Testing. Our Quality Department comprises 28 skilled QC inspectors. Functioning with an Integrated Manufacturer & Global Trading Hub background, our main markets are focused on the Middle East, South America, and Eastern Europe. We actively collaborate with 650 supply chain partners to serve diverse client groups, including cold storage operators, wholesale distribution chains, and automotive assembly facilities.
Driven by Intelligent Modular Racking Design, our innovation team provides flexible custom options such as corrosion-resistant galvanization, tailored column profiles, and adjustable beam heights. Last year, we successfully executed 28 new product releases, empowered by 18 R&D engineers.
Integrating robotic precision, automated profiling, and multi-stage testing to deliver top-tier structural stability.
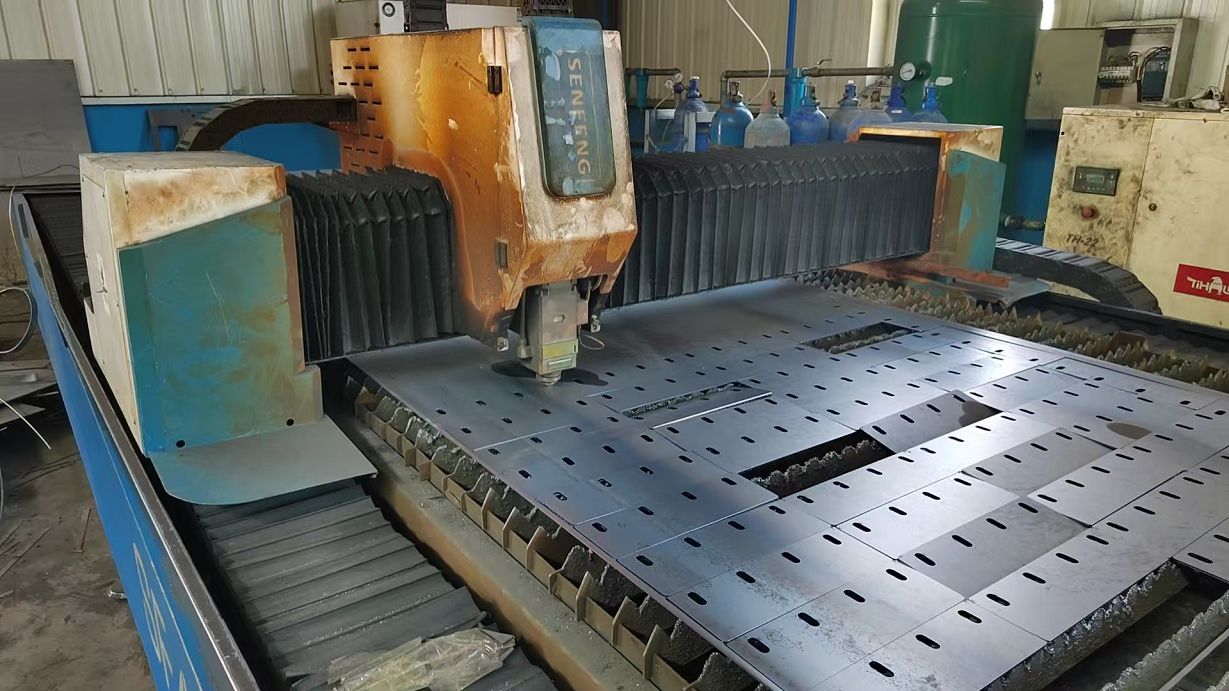
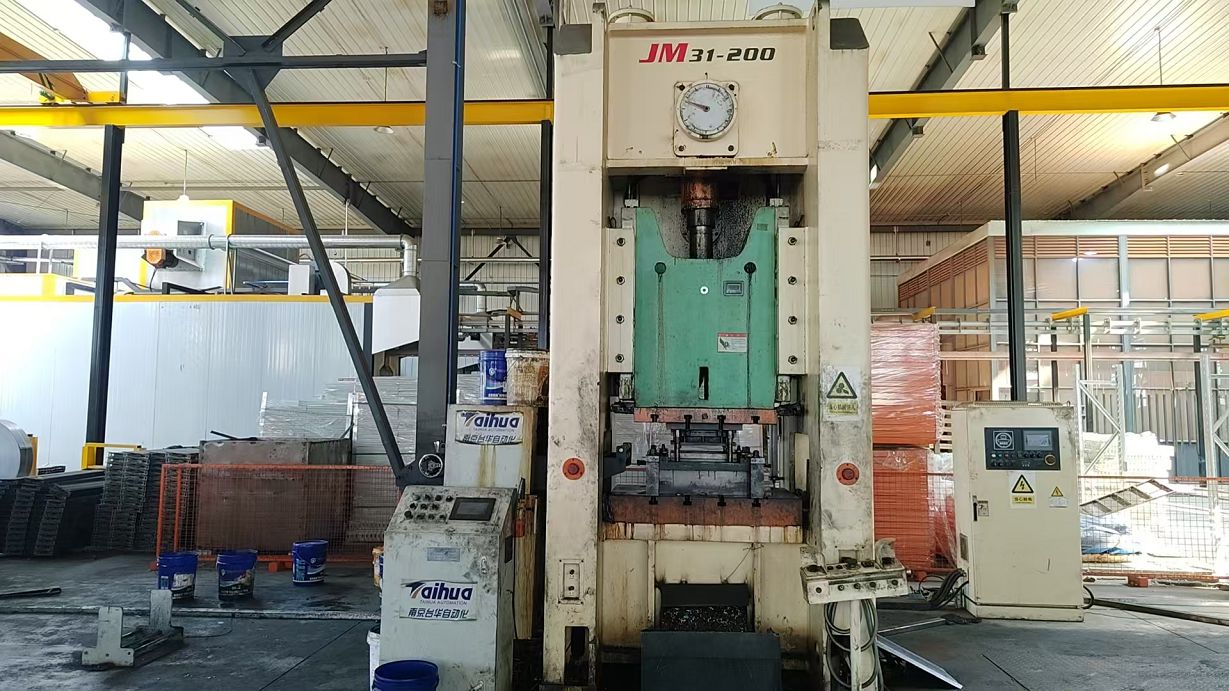
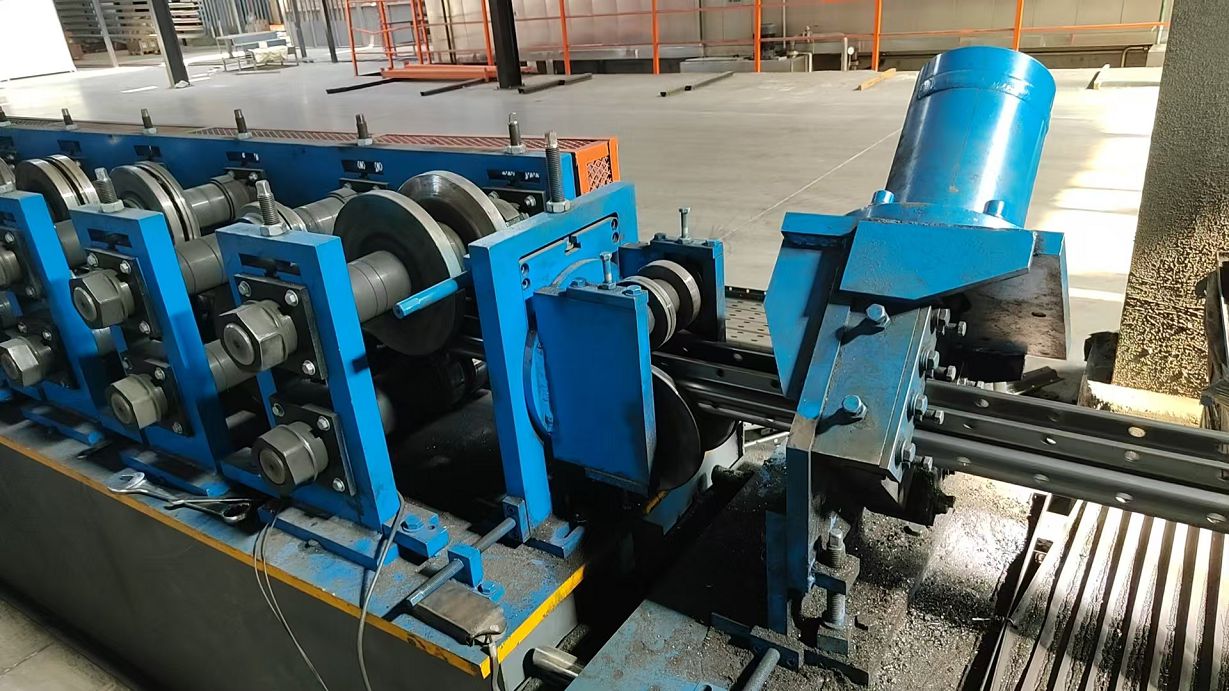
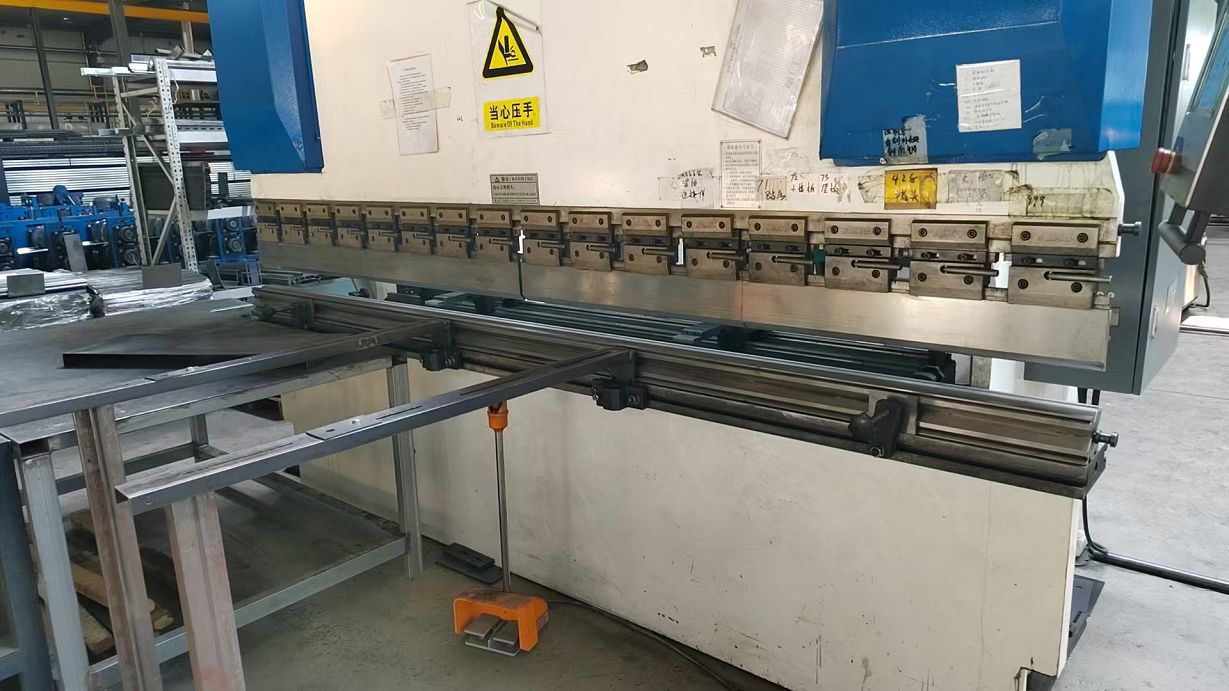
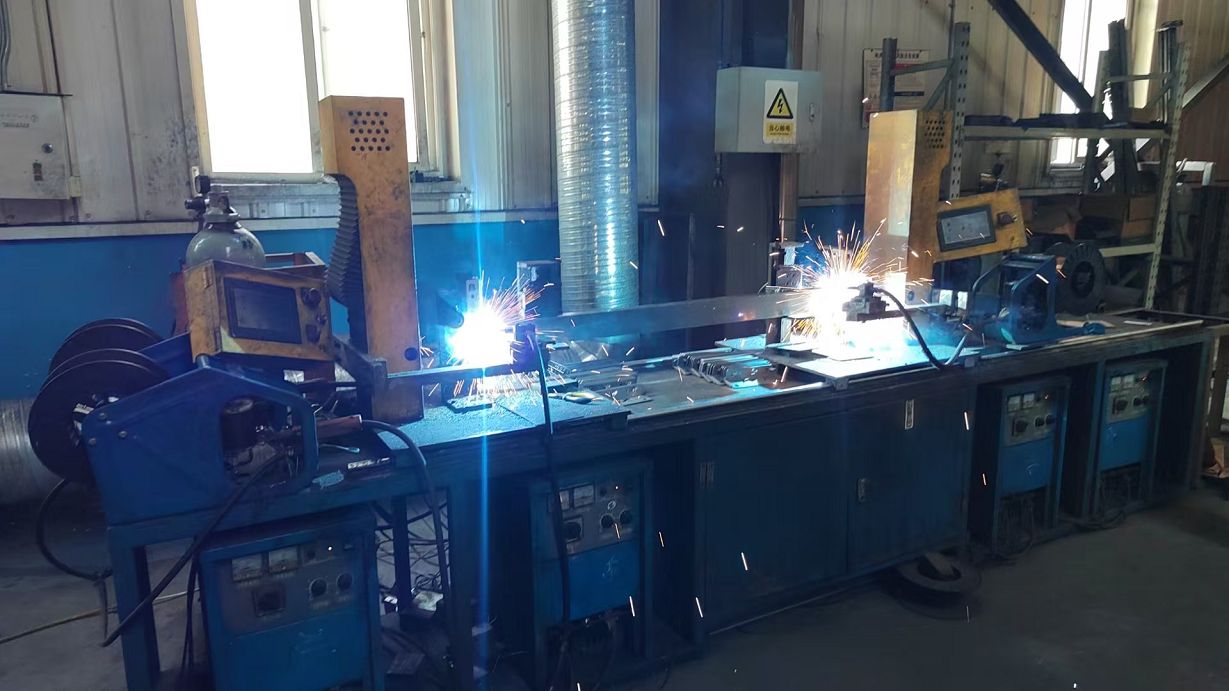
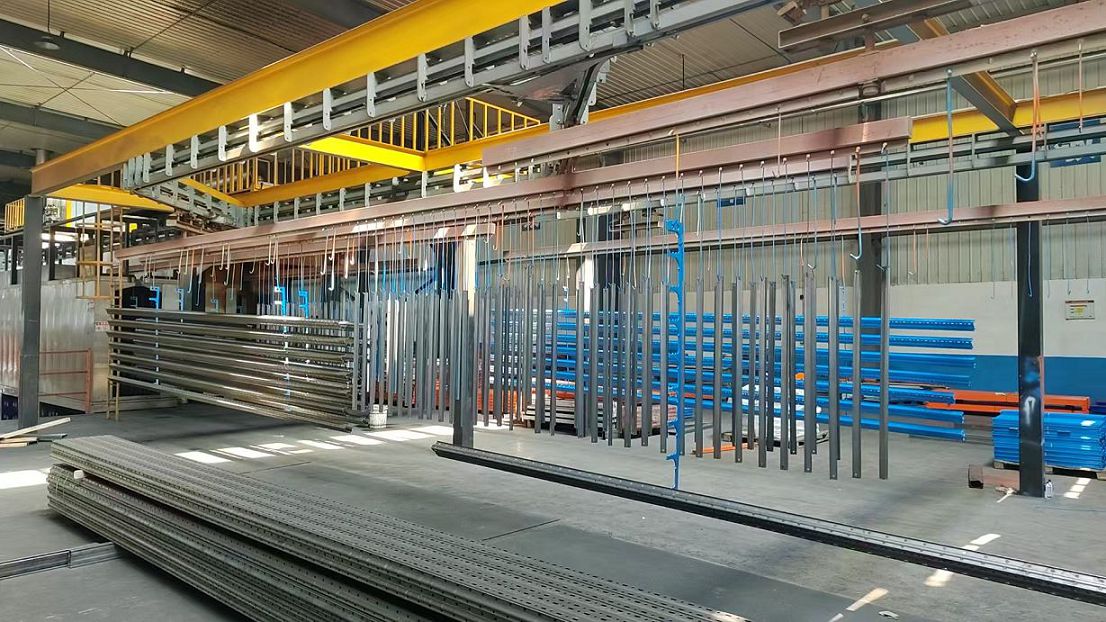
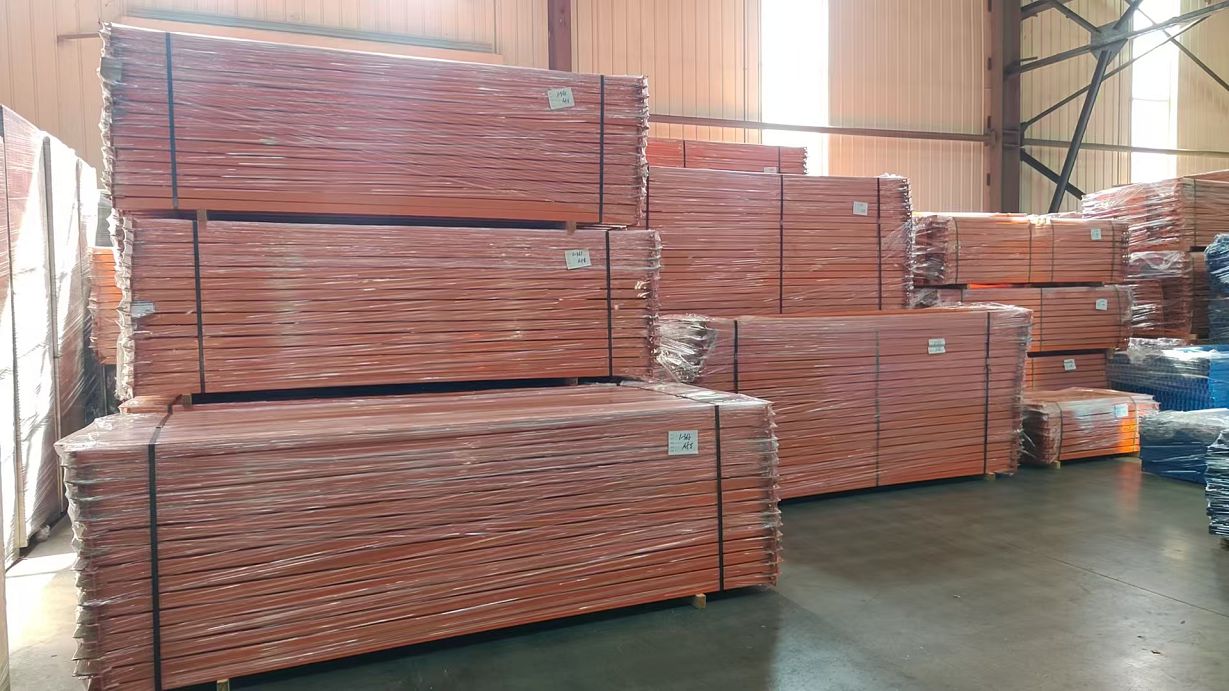
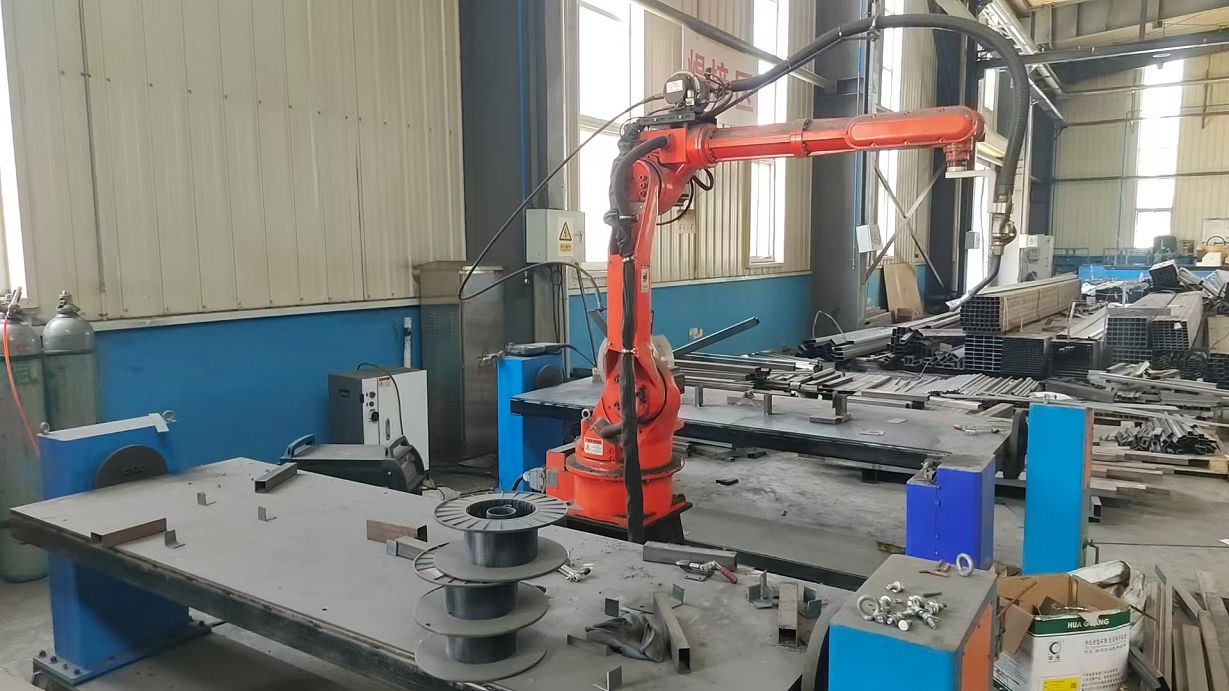
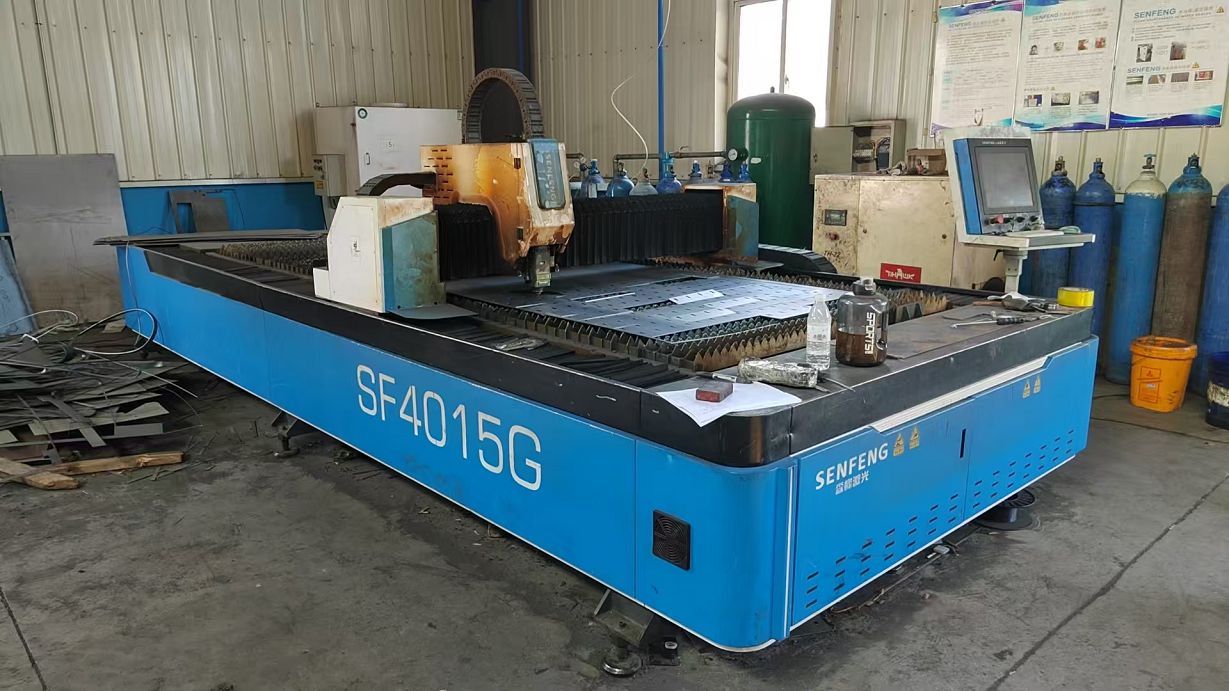
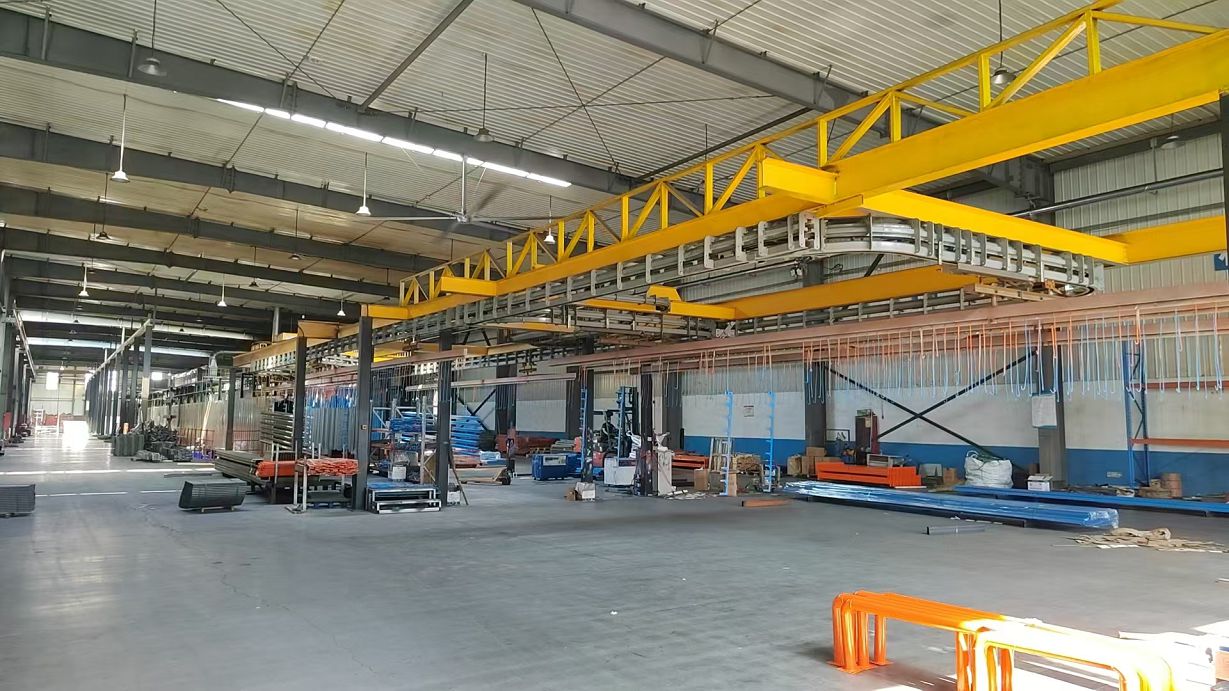
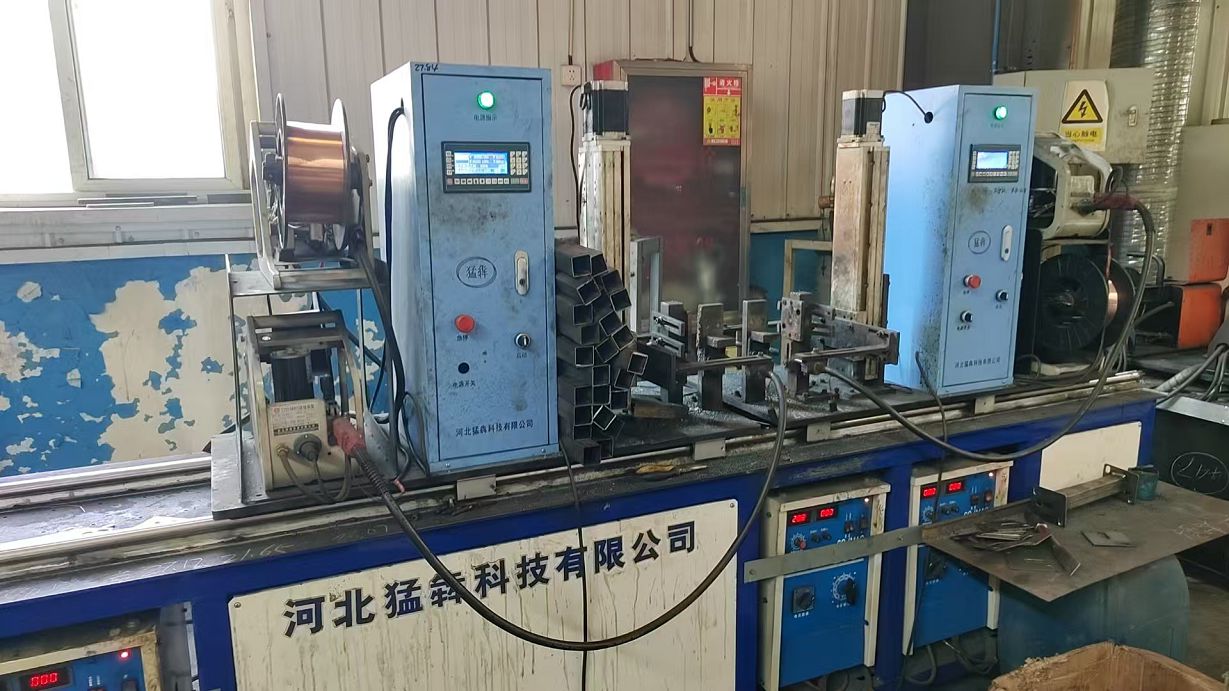
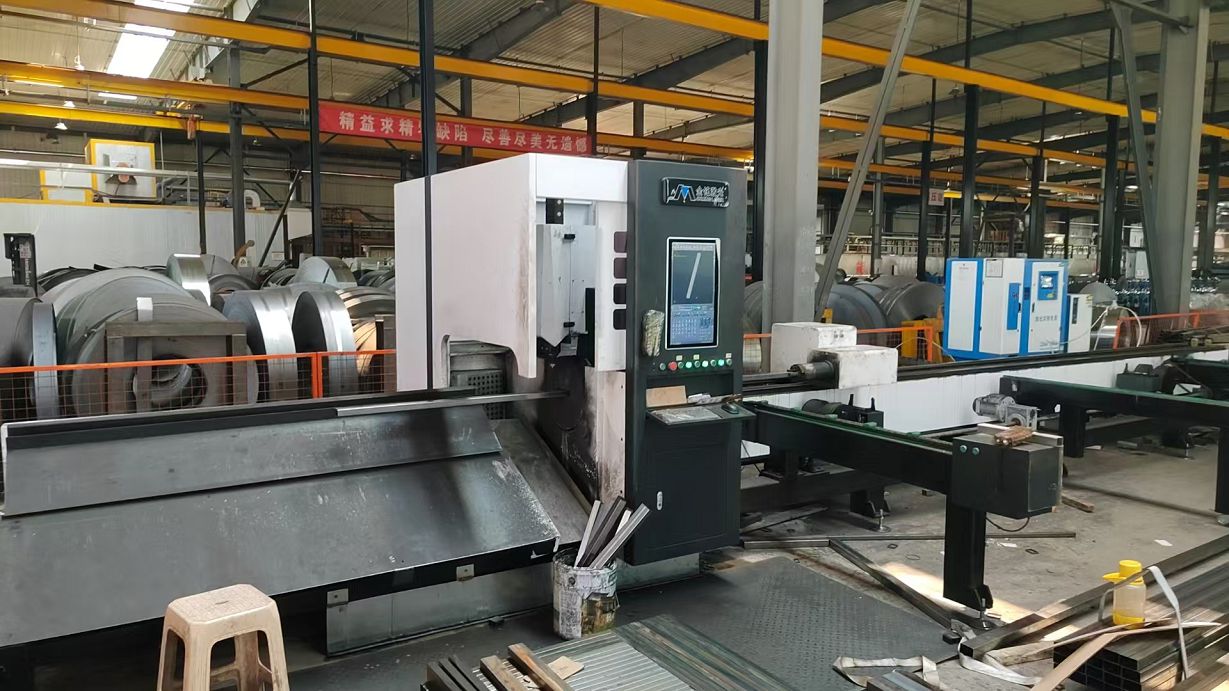
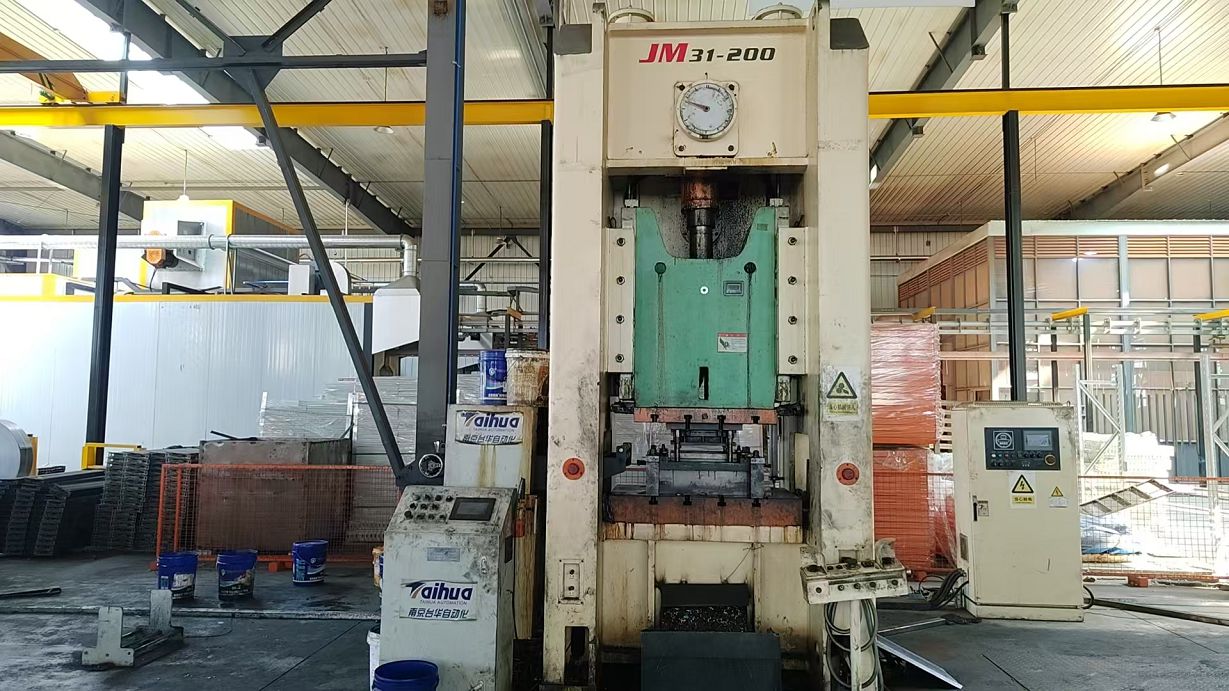
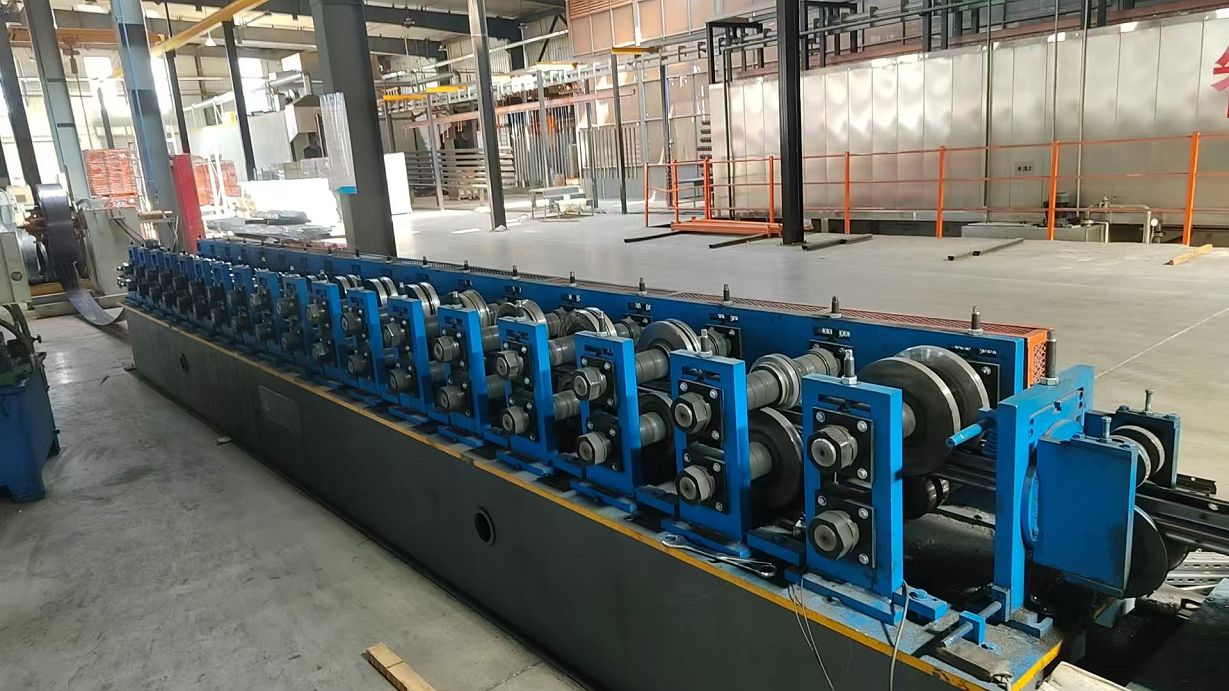
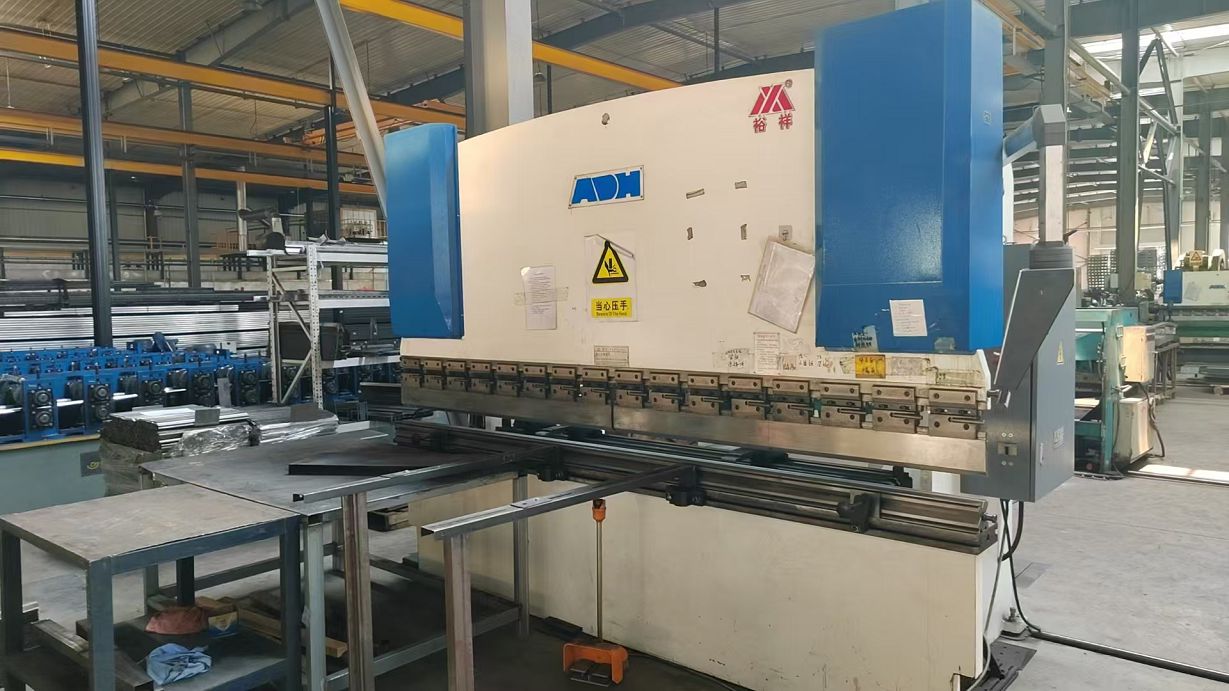
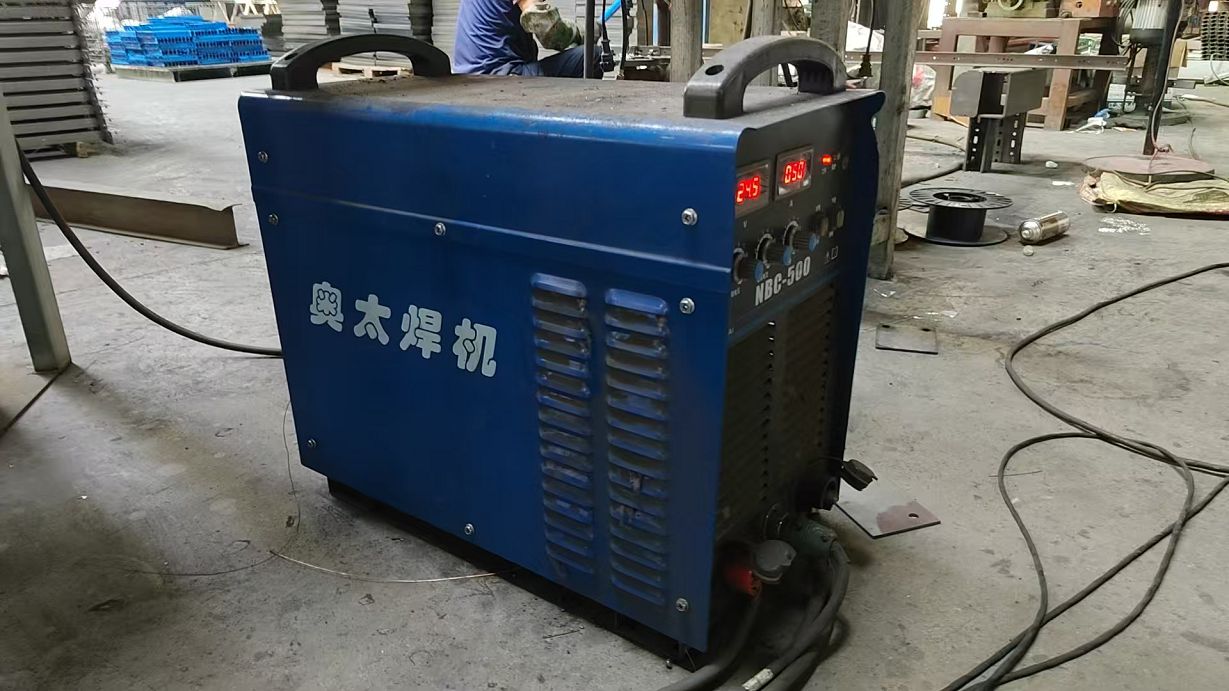
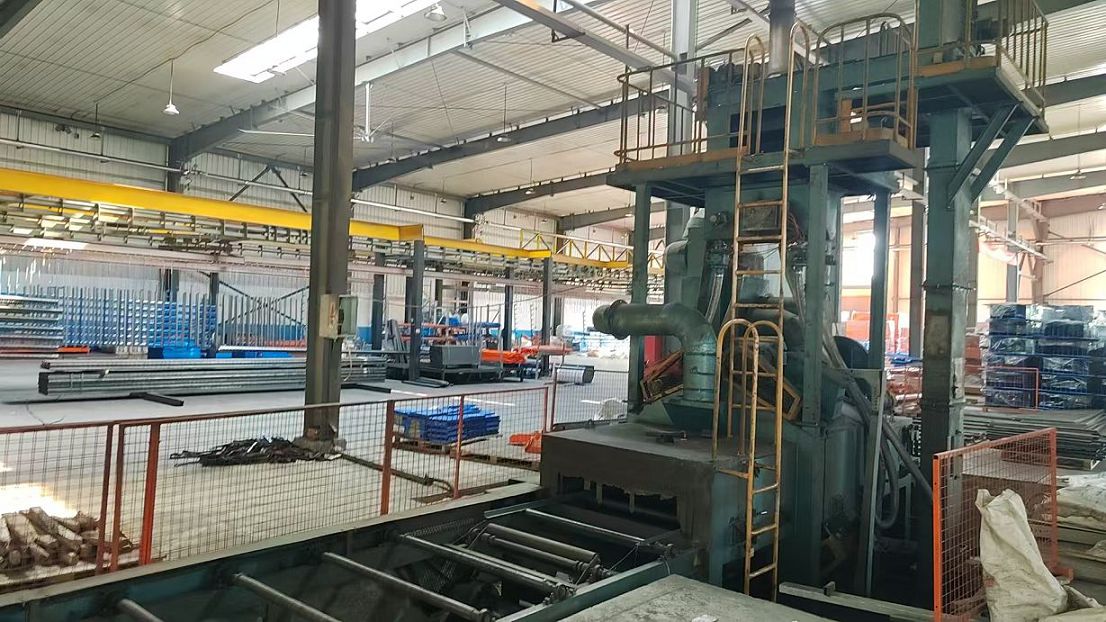
Different industrial environments demand tailored equipment specifications. Standard solutions rarely meet the distinct operating conditions of heavy warehousing or fast-moving retail settings:
Operating in environments down to -30°C requires specific metal selections and coating processes to prevent low-temperature steel embrittlement and peeling finish coats. Our specialized processes apply heavy-duty galvanization to keep structures functional for decades without structural decay.
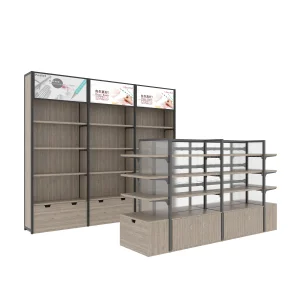
In retail settings with heavy foot traffic, checkout systems need integrated modular structures. Designing display layouts with impact-resistant bumpers and secure cable management systems reduces long-term maintenance costs and minimizes business downtime.
Storing heavy mechanical parts requires high load capacities. By using structural steel profiles with custom load distribution beams, assembly facilities can safely organize heavy components while optimizing floor space.
Helping procurement officers make informed, technical purchase decisions.
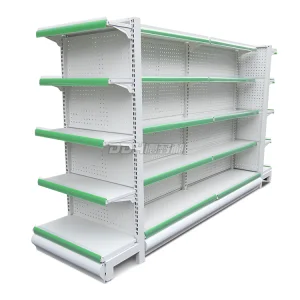
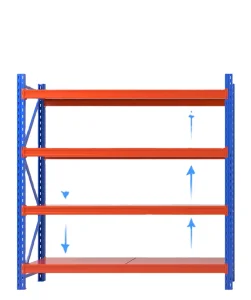
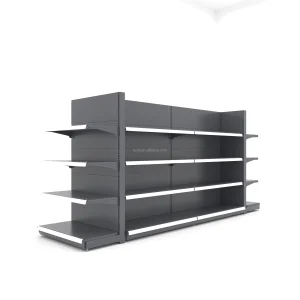
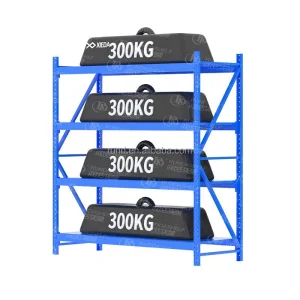
Explore our selection of heavy-duty industrial racking and modular display systems.
 CoreStorage